
Puncture-resistant vacuum packaging protects sensitive goods from oxygen, moisture, and contamination, yet packers frequently encounter frustrating micro-leaks and lost vacuum. A single ruptured pouch can ruin expensive chilled meats or trigger rust on precision metal components. You do not need to accept regular product loss as an inevitable cost of doing business.
Effective puncture-resistant vacuum packaging relies on balancing multi-layer film toughness, seal temperature windows, and edge geometry rather than simply adding film thickness. To stop leaks, processors must isolate whether failures stem from sharp points, transport friction, or improper sealing settings, and then validate customized multi-layer structures on their production machinery under actual distribution loads.
Selecting the right packaging requires moving beyond basic spec sheets and generic thickness ratings. Let us explore the engineering principles, failure analyses, and testing protocols that keep both sharp bone ends and heavy metal edges securely sealed.
Why Does Puncture-Resistant Vacuum Packaging Fail Despite Added Thickness?
Procurement teams often respond to vacuum loss by increasing bag thickness, but this approach routinely increases packaging costs without stopping customer returns. Added plastic gauge makes the pouch stiffer, which concentrates mechanical stress directly onto sharp product tips. You can eliminate packaging failures by diagnosing the precise physical mechanism behind the leak.
Puncture-resistant vacuum packaging fails when buyers mistake material thickness for mechanical toughness or seal integrity. Rigid thick films resist puncture poorly under dynamic flex, transfer impact forces to critical corners, and narrow the machine's thermal sealing window. True puncture resistance requires resilient polyamides, engineered tie-layers, and balanced thermal sealing properties working in harmony.
Deconstructing the Three Pillars of Vacuum Performance
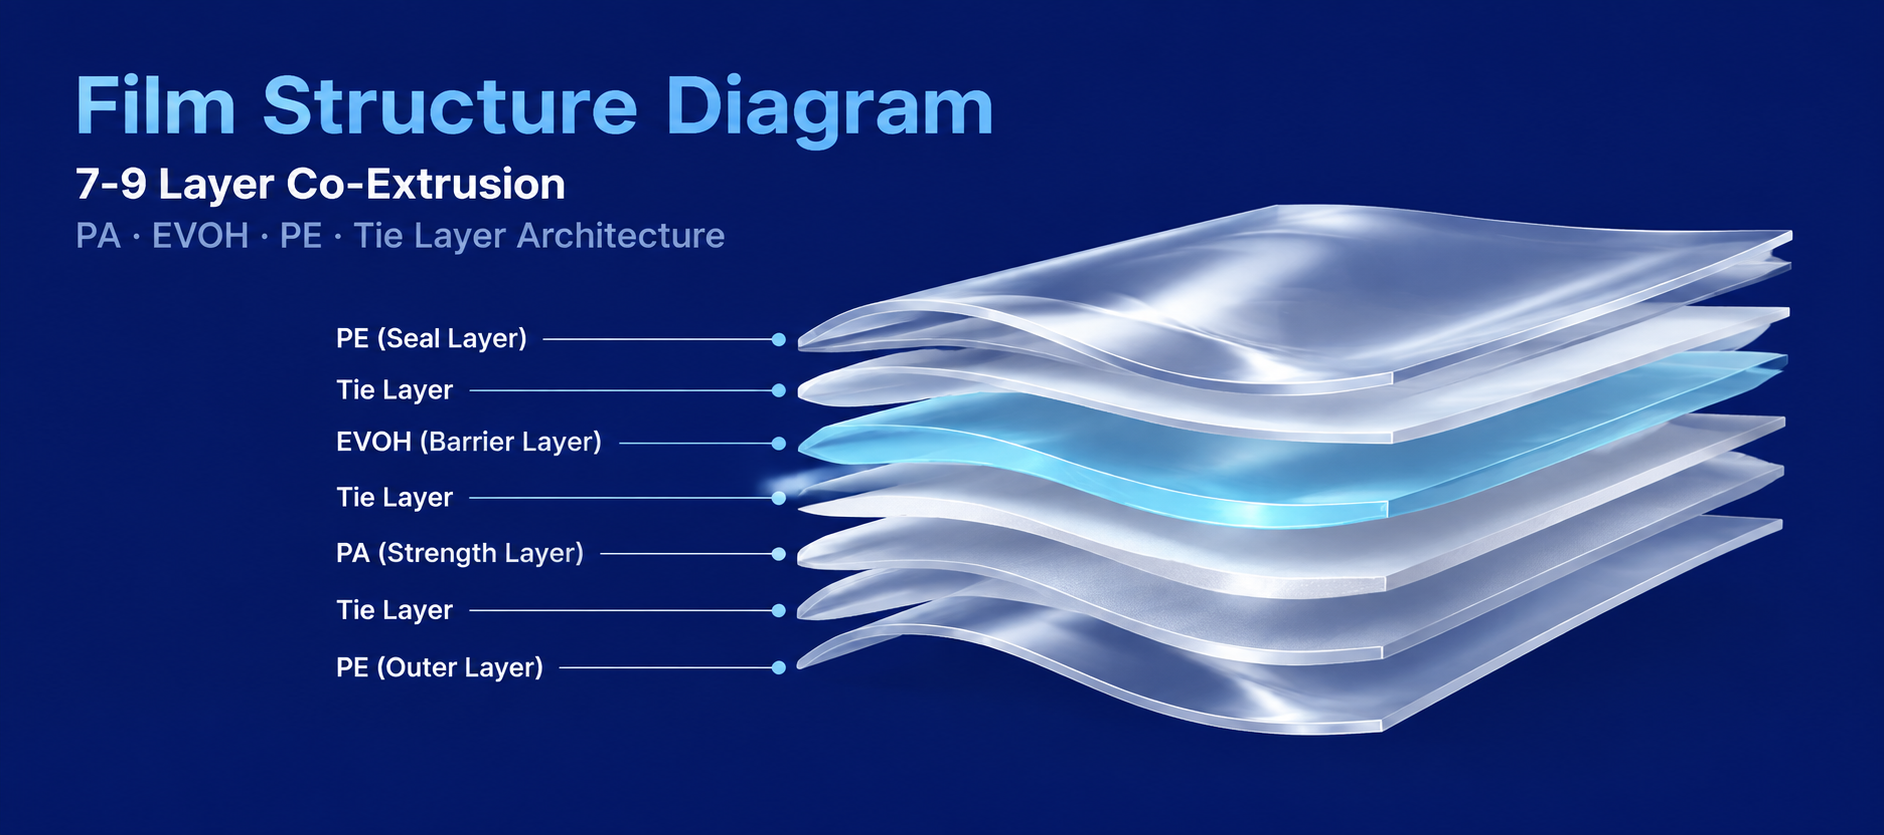
In our technical work at Qianxun New Material running 7-layer and 9-layer co-extrusion lines, we find that buyers frequently combine three separate packaging attributes into a single concept: puncture resistance, barrier performance, and seal integrity. Each function relies on distinct polymer layers within the co-extruded web:
- Puncture Resistance (Mechanical Core): Polyamide (PA/Nylon) provides high tensile strength, elongation, and puncture deflection. It absorbs mechanical point loads by stretching before tearing.
- Barrier Performance (Gas Exclusion): Ethylene Vinyl Alcohol (EVOH) stops oxygen transmission to preserve perishables and prevent industrial oxidation. However, EVOH is inherently brittle and offers minimal puncture resistance.
- Seal Integrity (Thermal Fusion): Polyethylene (PE) and ionomer sealants melt to fuse the package closed. If the seal layer is contaminated with animal fats or machine oils, or if the heat sealing jaws run too cold, the pack will lose vacuum regardless of its physical puncture rating.
ASTM Standards vs. Dynamic Packing Realities
Laboratory data sheets often report puncture values using static tests like ASTM F1306 (slow-rate penetration resistance) or ASTM D1709 (drop-dart impact). While these figures provide a baseline for raw resin quality, they do not simulate dynamic packing environments.
In a production line, vacuum draws the film tightly against sharp rib bones or threaded bolts. Then, the package undergoes vibration during transit. A stiff, 150-micron laminated bag may score high on a slow-puncture lab needle test, yet it can crack rapidly during a 1,000-mile freight run. The table below outlines how common film attributes perform under production pressures:
| Film Characteristic | Lab Test Indication | Real-World Failure Mode Under Vacuum | Recommended Structural Countermeasure |
|---|---|---|---|
| High Overall Thickness | High tensile yield (ASTM D882) | Corner fatigue, pinholing along fold lines | Lower gauge, switch to high-toughness multi-layer co-extrusion |
| Standard High-Barrier | Low OTR (ASTM D3985) | Brittle core fracture under point impact | Shield EVOH layers between symmetric PA shock absorbers |
| Standard PE Sealant | High seal strength (ASTM F88) | Seal failure over grease, moisture, or rust inhibitors | Modify sealant layer with metallocene PE for low-temp tack |
Thicker plastic is rarely the most cost-effective or reliable solution. Packaging engineers must evaluate how the film deflects under point loads and how the sealing interface handles process contamination.
How Does Puncture-Resistant Vacuum Packaging Differ Between Bone-In Meat and Industrial Parts?
Packaging managers frequently look for a single heavy-duty vacuum pouch to service diverse departments. Using an industrial-grade pouch for food—or vice versa—often causes costly hygiene non-compliance or unexpected mechanical punctures. Evaluating application-specific stress profiles is the only reliable way to prevent cross-category packaging failures.
Puncture-resistant vacuum packaging for meat requires food-contact compliance, low-temperature flex crack resistance, and fat-tolerant hermetic seals. In contrast, packaging for heavy industrial components demands high puncture modulus, extreme abrasion resistance against threaded corners, and chemical tolerance to surface corrosion-inhibiting oils.
The Bone-In Meat Environment: Cold, Wet, and Biological
Bone-in cuts—such as beef ribs, pork shoulders, and whole poultry—present distinct packaging challenges. The bone itself contains sharp ridges, but the surrounding product is soft and moist.
- Moisture and Lipids: Chilled meat expels blood, water, and animal fats. If any fat splatters into the seal area during loading, standard polyethylene seal layers fail to fuse. The packaging requires broad-temperature seal resins capable of sealing directly through grease.
- Cold-Chain Embrittlement: Food vacuum pouches operate under refrigeration (0°C to 4°C) or freezing (-18°C). Cold temperatures strip standard polyolefins of their ductility, making standard films brittle. Multi-layer structures with specialized PA grades maintain flexural fatigue resistance even at freezing temperatures.
- Hygiene and Microorganisms: Vacuum collapse pulls the film directly over bone shards. If a micro-puncture occurs, ambient oxygen enters and allows anaerobic or aerobic bacteria to proliferate, spoiling the meat without an obvious visual tear.
The Heavy Industrial Environment: Concentrated Mass, Abrasion, and Oils
Industrial components—such as machined flanges, threaded bolts, and steel stamping dies—interact with films in a purely mechanical way:
- High Mass and Point Inertia: Unlike compliant food items, industrial parts are rigid and dense. During transit, a 5-kilogram metal block shifts against the packaging floor. This movement creates abrasion and high shear forces that can strip internal layers.
- Threaded and Beveled Edges: Machine screw threads act as rows of small saws against the interior film surface. Packaging these parts requires high tensile modulus and surface hardness, preventing sharp edges from scoring the plastic.
- Processing Fluids: Finished metal parts are routinely coated with volatile corrosion inhibitors (VCI), stamping lubricants, or rust-preventative oils. The inner film layer must remain chemically inert so these fluids do not cause delamination or seal degradation.
Food processors and metal fabricators can share an evaluation methodology based on geometry, weight, and handling. However, they must never share a universal material specification.
What Can a Chicken Packaging Leak Investigation Teach Us About Sealing Integrity?
Processors often blame the packaging supplier for supplying "weak film" whenever vacuum losses spike on a packing line. In our engineering support visits, however, we find that assumed punctures often turn out to be machine-related sealing failures. A systematic diagnostic approach uncovers the true root cause and saves processors from unnecessary resin upgrades.
A joint investigation into leaking bone-in chicken pouches revealed that micro-voids in the seal—not bone punctures—caused the vacuum loss. While bone shards appeared to be the problem, fluctuating seal bar temperatures and animal grease contamination created micro-channels. Adjusting machine parameters and widening the thermal sealing window resolved the issue completely.
The Case: Leaking Pouches on a High-Speed Poultry Line
A commercial poultry processor packaging bone-in chicken portions approached our team at Qianxun New Material with a 7% line failure rate. Vacuum pouches were arriving at distribution centers soft, showing complete vacuum loss. The customer suspected that chicken bone fragments were puncturing the 90-micron multi-layer film. They requested a quote for a thicker 120-micron material.
Before changing the film thickness, we instituted a four-step failure analysis on their active packaging line:
[Inspect Field Rejects] ➔ [Submerge Bubble Testing] ➔ [Inspect Seal Cross-Sections] ➔ [Optimize Sealing Parameters]Step 1: Laboratory Submersion and Burst Testing
We took leaking pouches from the field and tested intact pouches from the same production lots. Using a vacuum leak chamber with dyed water (ASTM D3078), we submerged the packs and pulled a negative pressure.
- The Finding: Bubbles did not escape from the bone contact points. Instead, continuous streams of micro-bubbles emerged directly from the trailing edge of the heat seal.
Step 2: Seal Micro-Inspection
Under microscopic inspection, the film over the bone tips showed standard plastic deformation (cold drawing) without breaking through the skin. However, the heat-seal zone displayed incomplete resin flow. Droplets of chilled poultry fat were trapped in the seal seam, creating microscopic channels that opened under transit vibration.
Step 3: Sealing Machine Audit
We audited the customer's rotary vacuum chamber machine. The seal bars were set to a narrow operating window:
- Nominal Seal Temperature: 135°C
- Actual Bar Surface Temperature: Ranged from 121°C to 138°C across the full length of the jaw.
- Dwell Time: 1.1 seconds.
The seal bars were not maintaining consistent heat across all packing stations. When a bone positioned near the seal exerted mechanical leverage, the poorly fused, grease-contaminated seal peeled apart. The issue was seal failure, not material puncture.
The Resolution
Rather than increasing film thickness to 120 microns—which would have slowed heat transfer and worsened the cold-seal defect—we kept the film at 90 microns and modified the co-extruded formulation. We incorporated a high-performance metallocene-catalyzed sealant layer with superior hot-tack strength and an expanded sealing window (115°C to 155°C).
We also helped the client calibrate their heating elements and clean their sealing silicone strips. The line failure rate dropped from 7% to below 0.15% without increasing the client's film cost per unit.
How Should You Validate Puncture-Resistant Vacuum Packaging Before Full Production?
Switching packaging suppliers based solely on catalog specifications or lab tensile data exposes your supply chain to hidden risks. An off-the-shelf film might pass standard puncture tests but fail under your specific product geometries and line speeds. You can protect your bottom line by running physical prototyping trials that recreate your actual operating conditions.
You can validate puncture-resistant vacuum packaging by executing a phased qualification process: map product point severity, run sample pouches on your production sealers, conduct vacuum submersion checks, and complete real-world shipping distribution trials. This protocol confirms mechanical toughness, line throughput, and seal integrity before you commit to commercial orders.
Stage 1: Geometric and Load Profiling
Before requesting samples, audit the physical characteristics of the payload:
- Contact Geometry: Identify whether contact points are spherical, beveled, threaded, or needle-sharp.
- Weight Distribution: A 500-gram chicken leg acts differently than a 15-kilogram steel casting. Heavy objects require thicker lower layers to prevent dynamic puncture when dropped.
- Handling Temperatures: Note whether the pack will be blast-frozen, vacuum-sealed hot, or stored in humid outdoor warehouses.
Stage 2: Factory Machine Compatibility Trials
Never evaluate a sample pouch by manual inspection alone. Run trial rolls or pre-formed pouches directly on your operational vacuum packaging equipment:
- Load Real Product: Do not use foam blocks or smooth proxies. Use representative bone-in cuts or genuine machined parts.
- Test the Thermal Window: Intentionally run tests at the upper and lower limits of your machine's temperature settings (for example, ±10°C from target). A stable film should seal cleanly across that entire range.
- Check Evacuation Performance: Ensure the film conforms snugly around the product contours without bridging large air pockets across concave spaces.
Stage 3: Stress and Distribution Testing
Once sealed, samples must undergo mechanical stress tests that simulate real logistics:
[Sealed Vacuum Pack] ➔ [Drop Test (1.2m onto flat concrete)] ➔ [Vibration Table (ASTM D999)] ➔ [Vacuum Bubble Chamber (ASTM D3078)]If the package maintains vacuum after vibration and drop testing, inspect the contact points under magnification. Look for stress whitening (crazing), which indicates the polyamide layers are nearing their yield point.
Work closely with an experienced blown-film manufacturer who can adjust layer ratios—such as rebalancing PA, PE, and tie resins—to solve application-specific failure points before you order full production quantities.
Frequently Asked Questions
Does higher film thickness guarantee better puncture resistance?
No. Material composition matters more than total thickness. A flexible, multi-layer co-extruded film containing high-grade polyamide (Nylon) often outperforms a much thicker, standard low-density polyethylene film. Puncture resistance depends on the polymer's ability to stretch and dissipate impact energy rather than sheer bulk.
Can I use the same vacuum pouch for bone-in meat and metal hardware?
We do not recommend it. Food vacuum packaging requires certified direct-contact food safety compliance, cold-temperature crack resistance, and the ability to seal through fat or moisture. Industrial parts packaging prioritizes abrasion resistance, tear modulus, and tolerance to anti-rust oils. Each application requires dedicated layer structures.
What causes micro-leaks near the bag seal rather than on the body?
Micro-leaks near the seam are usually caused by incorrect sealing temperatures, inconsistent jaw pressure, or surface contaminants like grease, blood, or processing oils. If the heat seal layer cannot melt completely around these contaminants, microscopic channels remain, allowing air to leak back into the pouch over time.
How do EVOH and Polyamide (PA) layers differ in puncture-resistant vacuum packaging?
Polyamide (Nylon) provides mechanical strength, puncture resistance, and flex-crack durability. EVOH (Ethylene Vinyl Alcohol) provides an exceptional gas barrier against oxygen and odors, but it is physically brittle. High-performance vacuum films combine both materials, using tough polyamide layers to mechanically protect the delicate EVOH barrier core.
Conclusion
Selecting reliable puncture-resistant vacuum packaging is not a guessing game of adding thickness. True packaging performance depends on balancing layer-by-layer polymer toughness, machine sealing parameters, product edge geometry, and the stresses of real-world transit. Misdiagnosing a seal flaw as a puncture wastefully inflates material costs without curing the underlying failure.
At Qianxun New Material, our 7-layer and 9-layer co-extruded blow-molding technology enables us to engineer targeted barrier and puncture structures that secure sharp bones and dense industrial parts alike. Contact our technical team today to audit your failure modes, evaluate custom prototypes, and optimize your vacuum packaging performance.
Leave a Reply